
ASTM D395
Rubber Compression Set
Test Method A Compression Fixture
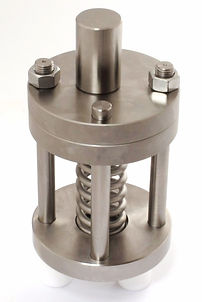
Test Method B Compression Fixture


Downloads: ASTM D395 - Standard Test Methods for Rubber Property—Compression Set - PDF · ASTM D395 Compression Platens – Universal Grip Data Sheet (PDF)
Written by Chris Thomas, Universal Grip Company · Reviewed by Frank Bertini · Updated October 17, 2026
ASTM D395 is the standard test method for rubber property, compression set. A disc of rubber is squeezed, held at temperature for a fixed time, released, allowed to recover, and measured; the thickness it fails to recover, expressed as a percentage, is the compression set. It is the number that tells a seal, gasket, O-ring, mounting or vibration damper buyer whether the part will still be pushing back after a year at service temperature, and it sits beside tensile (D412), tear (D624) and hardness in nearly every rubber specification.
The test looks simple, and that is why it is so often run wrong. This guide covers the three methods (constant force, constant deflection, and deflection by hardness), the Type 1 and Type 2 specimens and the spacer heights that set the deflection, the timing windows from cure to oven to measurement, the two different formulas and why the same compound gives a 4 % result by one and a 37 % result by the other, the fixture and die details, a realistic view of the precision, and how D395 maps to ISO 815-1 (including the release-method difference that can change a result by half). It ends with the fixtures, dies and machines Universal Grip supplies for the test.
In this guide: What ASTM D395 Measures · The Three Methods: A, B and C · Specimens: Type 1 and Type 2 · Fixture: Plates, Spacers and the Real Deflection · Time, Temperature and the Timing Windows · Step-by-Step Procedure (Method B) · Calculations and Worked Examples · Precision: What the Method Can Resolve · ASTM D395 vs ISO 815-1: The Release Method Matters · Common Errors · Equipment for ASTM D395 · FAQ
What ASTM D395 Measures
Compression set is the residual deformation of a rubber after it has been held under a compressive stress or strain and then released and allowed to recover. D395 defines it two ways, depending on the method: as a percentage of the original thickness (Method A, constant force), or as a percentage of the deflection that was applied (Methods B and C, constant deflection). The two are not interchangeable, and a result without the method letter attached is meaningless.
The property matters because rubber under compression does not stay elastic indefinitely. Physical relaxation of the polymer network, continued cross-linking, chain scission and oxidation at temperature all leave the material permanently shorter than it was. In a seal that means lost contact pressure and, eventually, leakage; in a mount it means sagging. Compression set at an elevated temperature over 22 or 70 hours is an accelerated proxy for that behaviour, and it is sensitive to cure state, filler loading and polymer type, which is why it is also used as a quality-control check on cure.
The scope is vulcanized rubber and thermoplastic elastomers in air (a liquid can be specified by agreement). Low-temperature compression set, where the question is crystallisation and glass transition rather than ageing, is a separate standard, ASTM D1229. Cellular rubber and foams have their own set tests (ASTM D1056 and D3574); O-rings are tested by the D395 methods through ASTM D1414. The current edition is D395-18, reapproved in 2025. See our elastomer testing page for how it fits into a rubber lab.
The Three Methods: A, B and C
-
Method A, compression set under constant force: the specimen is loaded by a calibrated spring that applies 1.8 kN (400 lbf) throughout the test. The deflection is whatever the rubber takes under that force, so softer compounds are squeezed more. Set is reported as a percentage of the original thickness.
-
Method B, compression set under constant deflection: the specimen is compressed between parallel plates to a fixed height set by spacer bars, approximately 25 % deflection, and held there. Set is reported as a percentage of the applied deflection. This is the default: the standard says Method B is used unless a detailed specification says otherwise, and it is the method almost every specification and data sheet means by "compression set".
-
Method C, constant deflection with deflection chosen by hardness: the same plate-and-spacer principle as Method B, but the deflection is set from the IRHD hardness of the compound: 25 ± 2 % for hardness up to 80 IRHD, 15 ± 2 % for 81 to 89, and 10 ± 1 % for 90 and above. It exists because hard compounds cannot be compressed 25 % without damage; Method B is not suitable above 90 IRHD. Method C mirrors the strain selection in ISO 815-1.
Some competitor pages describe Method B as a "constant pressure" test. It is the opposite. The strain is fixed; the stress decays throughout the test as the rubber relaxes. If the question is how much force the part is still exerting, that is stress relaxation (ASTM D6147), not compression set.
Specimens: Type 1 and Type 2
-
Type 1: a cylindrical disc 12.5 ± 0.5 mm thick and 29.0 ± 0.5 mm in diameter (0.49 × 1.14 in). Used for Methods A, B and C. The 12.9 mm thickness quoted on one widely read materials database is wrong.
-
Type 2: a disc 6.0 ± 0.2 mm thick and 13.0 ± 0.2 mm in diameter (0.24 × 0.51 in). Methods B and C only; it is the specimen for thin sheet and small parts.
-
Preparation: die-cut from sheet prepared per ASTM D3182 and D3183, or molded to size. Discs may be plied up without cement to reach the thickness, up to 7 discs for Type 1 or 4 for Type 2, but plied specimens do not necessarily give the same result as solid ones and the construction must be reported.
-
Number: two specimens with the average reported, or three with the median reported. State which option was used.
-
Thickness measurement: at the centre of the disc per ASTM D3767, to the nearest 0.02 mm (0.001 in). For compounds under 35 IRHD the gauge foot force is reduced to 0.2 ± 0.05 N so the foot does not sink into the rubber.
A sharp 29.0 mm or 13.0 mm cutting die in a die press gives a clean cylinder with square edges; a ragged or barrel-shaped edge changes the effective area and the thickness reading. Buffed specimens must rest at least 30 minutes before cutting.
Fixture: Plates, Spacers and the Real Deflection
The Method B and C fixture is a stack of two or more flat steel plates, hard-chrome plated and ground to a surface roughness of 0.250 µm Ra or better, with spacer bars between them and bolts to pull the plates down until they rest on the spacers. The plates must be stiff enough not to bend under the rubber's reaction; the standard warns against over-tightening the bolts for that reason, and the bolts are tightened evenly, in sequence, until the plates just contact the spacers.
-
Spacers for Type 1: 9.5 ± 0.02 mm (0.375 ± 0.001 in). On a nominal 12.5 mm disc that is 24 % deflection; with the specimen thickness tolerance the actual deflection ranges from about 20 to 26 %. The standard says "approximately 25 %" for this reason.
-
Spacers for Type 2: 4.50 ± 0.01 mm (0.1770 ± 0.0005 in), giving 25 % nominal and 23 to 29 % with tolerances.
-
Method C spacers: chosen to give 25, 15 or 10 % of the measured specimen thickness; an alternative Method C device with an integral micrometer sets the compressed height directly to 0.75, 0.85 or 0.90 of the original thickness.
-
Lubricant: a thin film of a fluid with no action on the rubber (silicone or fluorosilicone fluid) may be applied to the plates to prevent the disc gripping them; it is optional and must be reported.
-
Capacity: a plate stack is normally sized for several discs per gap, so one fixture holds a set of two or three specimens for each of two or three compounds. Three spacers per gap, placed around the discs, keep the plates parallel.
The Method A device is a different animal: a calibrated spring with a stiffness of 70 ± 3.5 kN/m at the 1.8 kN load, a solid (fully compressed) force of at least 2.4 kN, and a fatigue requirement that it change by no more than 0.3 mm after a week at 70 °C under load. The plates are the same chrome-plated steel. Few labs own one; most Method A work is now done with the spring device only when a specification demands it.
Universal Grip's compression set fixtures are chrome-plated, ground plate stacks with Type 1 and Type 2 spacer sets and multi-specimen capacity; see the compression fixtures page for sizes and the compression platens used for Method A or D575 work on a universal testing machine.
Time, Temperature and the Timing Windows
D395 is as much a schedule as a test. The windows below are the ones that are most often missed, and each one changes the result.
-
After cure: test no sooner than 24 hours and no later than 60 days after vulcanization (60 days from receipt if the cure date is unknown). Freshly cured rubber is still cross-linking and gives a high set.
-
Before test: condition at least 3 hours at 23 ± 2 °C; moisture-sensitive compounds at least 24 hours at 50 ± 10 % RH.
-
Into the oven: the assembled, loaded fixture must go into the oven within 2 hours of assembly.
-
Duration: 22 hours and 70 hours are the suggested periods; 22 to 24 h, 70 to 72 h, 166 to 168 h or multiples are all permitted. Report the one used.
-
Temperature: from the ASTM D1349 list of standard temperatures (23, 27, 40, 55, 70, 85, 100, 125, 150, 175, 200, 225 and 250 °C). 70 °C is the historic general-purpose condition, 100 °C the common NBR condition, 125 °C typical for EPDM, 150 °C for HNBR and 200 °C for fluoroelastomers. The oven is an ASTM E145 Type IIB (to 70 °C) or Type IIA gravity or forced-draft oven with an interior of at least 300 mm cube.
-
Recovery: remove the fixture from the oven, release the specimens immediately, and let them rest for 30 minutes on a poor thermal conductor such as wood at 23 ± 2 °C before measuring. Measuring early reads high; rubber keeps recovering for hours.
The 30-minute recovery is the one most often shortened in a busy lab, and it is also the point where D395 and ISO 815-1 diverge (see below).
Step-by-Step Procedure (Method B)
-
1. Cut or mold two or three discs of the type required, at least 24 hours after cure. Inspect edges.
-
2. Condition 3 hours at 23 ± 2 °C and measure the original thickness t0 of each disc at its centre to 0.02 mm.
-
3. Assemble the fixture: discs centred between the plates, spacers around them, optional lubricant film, bolts tightened evenly until the plates touch the spacers. Record the spacer height tn.
-
4. Oven: within 2 hours of assembly, place the fixture in the oven at the test temperature and start the clock.
-
5. Hold for 22 h (or 70 h, or the specified period).
-
6. Release: remove the fixture, open it at once and lay the discs on a wooden board at room temperature.
-
7. Measure the recovered thickness ti of each disc after 30 minutes, at the centre, to 0.02 mm.
-
8. Calculate the set for each disc and report the average of two or the median of three, with method, specimen type, time, temperature and any lubricant or plying.
For Method A, replace the spacer stack with the spring device loaded to 1.8 kN; for Method C, measure IRHD hardness first and select the spacer or micrometer setting from the 25/15/10 % rule.
Calculations and Worked Examples
-
Method A: C A = (t0 − ti) ÷ t0 × 100, where t0 is the original thickness and ti the thickness after recovery.
-
Methods B and C: C B = (t0 − ti) ÷ (t0 − tn) × 100, where tn is the spacer thickness. The denominator is the deflection that was applied, not the whole thickness.
Worked example, Method B, Type 1. A disc measures t0 = 12.50 mm. The Type 1 spacers are tn = 9.50 mm, so the applied deflection is 3.00 mm. After 22 hours at 100 °C and 30 minutes of recovery the disc measures ti = 11.40 mm. Compression set = (12.50 − 11.40) ÷ (12.50 − 9.50) × 100 = 1.10 ÷ 3.00 × 100 = 36.7 %. The second disc gives 35.1 %; the reported Method B value is the average, 35.9 %.
Worked example, Method A, same compound. A disc of t0 = 12.52 mm is held under the 1.8 kN spring for 22 hours at 100 °C and recovers to ti = 12.05 mm. Compression set = (12.52 − 12.05) ÷ 12.52 × 100 = 0.47 ÷ 12.52 × 100 = 3.8 %. The two numbers describe the same rubber: Method A divides by the full 12.5 mm thickness, Method B divides by the 3 mm deflection, so a Method B value is naturally several times larger. Comparing a 4 % Method A figure on one data sheet with a 37 % Method B figure on another says nothing about which compound is better.
Worked example, Type 2. t0 = 6.02 mm, tn = 4.50 mm (deflection 1.52 mm), ti = 5.71 mm. Set = (6.02 − 5.71) ÷ 1.52 × 100 = 0.31 ÷ 1.52 × 100 = 20.4 %. Note how a 0.02 mm reading error on a Type 2 disc moves the result by 1.3 percentage points, against 0.7 points on a Type 1 disc; the small specimen is more sensitive to measurement.
Typical values. General-purpose compounds at 70 °C for 22 hours commonly fall between 15 and 35 % by Method B; good sealing grades 8 to 20 %; silicones 10 to 30 % at 100 °C. Specification limits are usually written at a specific time and temperature, for example 40 % maximum after 72 hours at 100 °C for a 70 Shore A NBR O-ring grade in ISO 3601-5. A set above 100 % is possible on an undercured compound that continues to cure and shrink in the oven; it is a signal of cure state, not a measurement error.
Precision: What the Method Can Resolve
D395 includes interlaboratory precision data, and the headline is that reproducibility between laboratories is roughly 30 % of the mean. For Method B on Type 1 specimens, one material with a mean of 13.7 % had a within-laboratory repeatability of 1.7 points (12 % of the mean) and a between-laboratory reproducibility of 4.4 points (32 % of the mean); a second material at 52.8 % mean had repeatability of 1.6 points and reproducibility of 16.8 points. Method A gave similar relative figures. There is no bias statement because there is no reference material.
Two practical consequences follow. A specification limit of, say, 25 % maximum cannot resolve the difference between a compound that tests at 23 % in one lab and 27 % in another; both labs can be running the method correctly. And a supplier and customer who disagree on a compression set result should compare timing, release and recovery details before they compare compounds. Within one lab, the method is much tighter, which is why compression set works well as a cure-state trend check and poorly as a referee test.
ASTM D395 vs ISO 815-1: The Release Method Matters
ISO 815-1 (2019, confirmed 2025) is the international equivalent and is close enough that many labs treat the two as the same. The differences are small in geometry and large in procedure.
-
Specimens: ISO Type A is 29.0 ± 0.5 × 12.5 ± 0.5 mm, identical to D395 Type 1. ISO Type B is 13.0 ± 0.5 × 6.3 ± 0.3 mm, 0.3 mm thicker than D395 Type 2 with looser tolerances.
-
Strain: 25 ± 2 % for 10 to 80 IRHD, 15 ± 2 % for 80 to 89, 10 ± 1 % for 90 to 95, which is what D395 Method C adopts; D395 Method B simply uses the 25 % spacers regardless of hardness up to 90 IRHD.
-
Duration: 24 h with a −2 h allowance (so 22 to 24 h, effectively the same window as D395's 22 h), 72 h and 168 h.
-
Release method: this is the big one. ISO 815-1 defines three. Method A releases the specimen hot and measures after 30 ± 3 minutes at room temperature, which is what D395 does. Method B cools the still-loaded fixture to 23 °C over 30 to 120 minutes, then releases and measures after 30 minutes; the rubber sets further while cooling under load ("cold set") and the result is highest. Method C releases the specimen inside the oven, lets it recover hot for 30 minutes, then cools it for 30 minutes; the result is lowest. Published data on one NBR-type compound at 72 h/100 °C gave 14 % by hot release and 21 % with the fixture cooled under load, a 50 % difference from the release method alone.
So an ISO 815-1 result is comparable to a D395 result only if ISO release method A was used, and a report that does not state the release method is incomplete. Low-temperature set is ISO 815-2 and ASTM D1229 respectively.
Common Errors
-
Reporting a result without the method letter, or applying the Method A formula (divide by t0) to a Method B test.
-
Calling the test "25 % deflection" and then cutting spacers at 25 % of the measured thickness instead of using the 9.5 mm or 4.50 mm bars the standard specifies.
-
Testing within 24 hours of cure, or more than 60 days after it.
-
More than 2 hours between assembling the fixture and putting it in the oven.
-
Measuring before the 30-minute recovery is up, or measuring on a metal bench that chills the disc.
-
Over-tightening the bolts and bowing the plates, so the discs nearest the bolts are compressed more than those in the middle.
-
Discs stuck to the plate and torn on release; use the permitted lubricant film and include any release film thickness in the spacer height.
-
Measuring off-centre, or with the full gauge foot force on a very soft compound.
-
Comparing a D395 result with an ISO 815-1 result obtained by release method B.
-
Writing a specification limit tighter than the ±30 % reproducibility of the method.
Equipment for ASTM D395
-
Fixtures: compression set fixtures with chrome-plated ground plates, Type 1 (9.5 mm) and Type 2 (4.50 mm) spacer sets and multi-disc capacity; Method C spacer sets to order.
-
Specimen preparation: 29.0 mm and 13.0 mm cutting dies and a die press for clean cylindrical discs, plus a D3767 thickness gauge with the reduced-force foot for soft compounds.
-
Method A and related compression tests: compression platens on a benchtop universal testing machine or a Mark-10 tensile tester for load-controlled compression, ASTM D575 compression stress-strain and D1414 O-ring work.
-
Oven: an ASTM E145 air oven (not an environmental chamber) for the hold period; environmental chambers are for in-frame tests such as D575 at temperature.
-
Companion tests on the same bench: ASTM D412 tensile, D624 tear and durometer hardness, which together with compression set make up the basic rubber specification set.
For a complete rubber lab configuration see the elastomers testing page.
ASTM D395 FAQ
What is ASTM D395?
The ASTM standard test method for compression set of rubber. A disc is compressed, held at temperature for 22 or 70 hours, released and allowed to recover for 30 minutes; the thickness it fails to recover, as a percentage of the original thickness (Method A) or of the applied deflection (Methods B and C), is the compression set.
What are the ASTM D395 specimen sizes?
Type 1 is a disc 12.5 ± 0.5 mm thick and 29.0 ± 0.5 mm in diameter, used for Methods A, B and C. Type 2 is 6.0 ± 0.2 mm thick and 13.0 ± 0.2 mm in diameter, for Methods B and C only. Two specimens are averaged or three are reported as the median.
What is the difference between Method A and Method B?
Method A holds the specimen under a constant force of 1.8 kN from a calibrated spring and reports set as a percentage of original thickness. Method B holds it at a constant deflection of approximately 25 % set by spacer bars and reports set as a percentage of that deflection. Method B is the default unless a specification says otherwise.
What is Method C in ASTM D395?
A constant-deflection test in which the deflection is chosen from the compound's IRHD hardness: 25 % up to 80 IRHD, 15 % for 81 to 89, and 10 % for 90 and above. It is used for hard compounds that cannot take the 25 % deflection of Method B.
What spacer thickness does ASTM D395 use?
9.5 ± 0.02 mm for Type 1 specimens and 4.50 ± 0.01 mm for Type 2. On nominal specimens that is 24 % and 25 % deflection; with specimen tolerances the real deflection is 20 to 26 % (Type 1) and 23 to 29 % (Type 2), which is why the standard says approximately 25 %.
How is compression set calculated?
Method A: (t0 − ti) ÷ t0 × 100. Methods B and C: (t0 − ti) ÷ (t0 − tn) × 100, where t0 is the original thickness, ti the thickness after 30 minutes of recovery and tn the spacer thickness. The Method B denominator is the deflection, so Method B values are several times larger than Method A values for the same rubber.
What time and temperature does ASTM D395 use?
22 hours or 70 hours are the suggested periods (22–24, 70–72 and 166–168 h are permitted) at a temperature from the ASTM D1349 list: 70 °C is the historic default, with 100, 125 and 150 °C common for NBR, EPDM and HNBR respectively, and 200 °C for fluoroelastomers.
How long is the recovery period in ASTM D395?
30 minutes at 23 ± 2 °C on a poor thermal conductor such as wood, after releasing the specimen immediately on removal from the oven. Thickness is then measured at the centre to 0.02 mm.
How soon after molding can compression set be tested?
Not sooner than 24 hours and not later than 60 days after vulcanization, after at least 3 hours of conditioning at 23 ± 2 °C. The loaded fixture must go into the oven within 2 hours of assembly.
What is a good compression set value?
It depends on the condition. By Method B at 70 °C for 22 hours, general-purpose compounds commonly fall between 15 and 35 % and good sealing grades between 8 and 20 %; silicones run 10 to 30 % at 100 °C. Specification limits are tied to a stated time and temperature, so a value without those conditions cannot be judged.
What is the difference between ASTM D395 and ISO 815-1?
The Type A/Type 1 specimens are identical and the 24 h and 22 h windows overlap, but ISO Type B is 6.3 mm thick (D395 Type 2 is 6.0 mm) and ISO 815-1 defines three release methods. Only ISO release method A (release hot, measure after 30 minutes) matches D395; method B (cool the loaded fixture first) can give a result 50 % higher on the same compound.
How repeatable is ASTM D395?
Within a laboratory, repeatability is roughly 3 to 12 % of the mean. Between laboratories the reproducibility is about 30 % of the mean, so a 25 % limit cannot distinguish a 23 % result in one lab from a 27 % result in another. Timing, release and recovery details drive most of the difference.
Need a fixture, grips or a complete system for ASTM D395? Contact Universal Grip with your specimen details, capacity and machine connection and we will quote the right setup.